






For casthouses, we build the line from melting to homogenisation
Billet quality is determined before the moment of casting, in the furnace: the melting regime, the stability of the holding temperature, the removal of gas and inclusions. From the melting furnace to degassing, and from vertical casting to homogenisation, we engineer the line under single-source responsibility.
Every degree in the furnace stays inside the billet
If the temperature in the holding furnace swings by a few degrees, this directly affects the casting speed and the internal structure of the billet. Likewise, if degassing is insufficient, the defect does not show during casting; it appears at the extrusion press or in the customer’s hands. That is why we treat the melting, holding, degassing and casting steps not as separate pieces of equipment but as a single process chain.
At the PMS Aluminium plant in Bursa we built this chain on a turnkey basis: design, manufacturing, installation and commissioning all stayed with us, and the stations were delivered not as separate pieces of equipment but as a single production line. At Kurtoğlu Aluminium we engineered the casting line and the homogenising furnace together — the step that determines the thermal history of the billet cannot be considered apart from the casting line.
Explore the PMS Aluminium project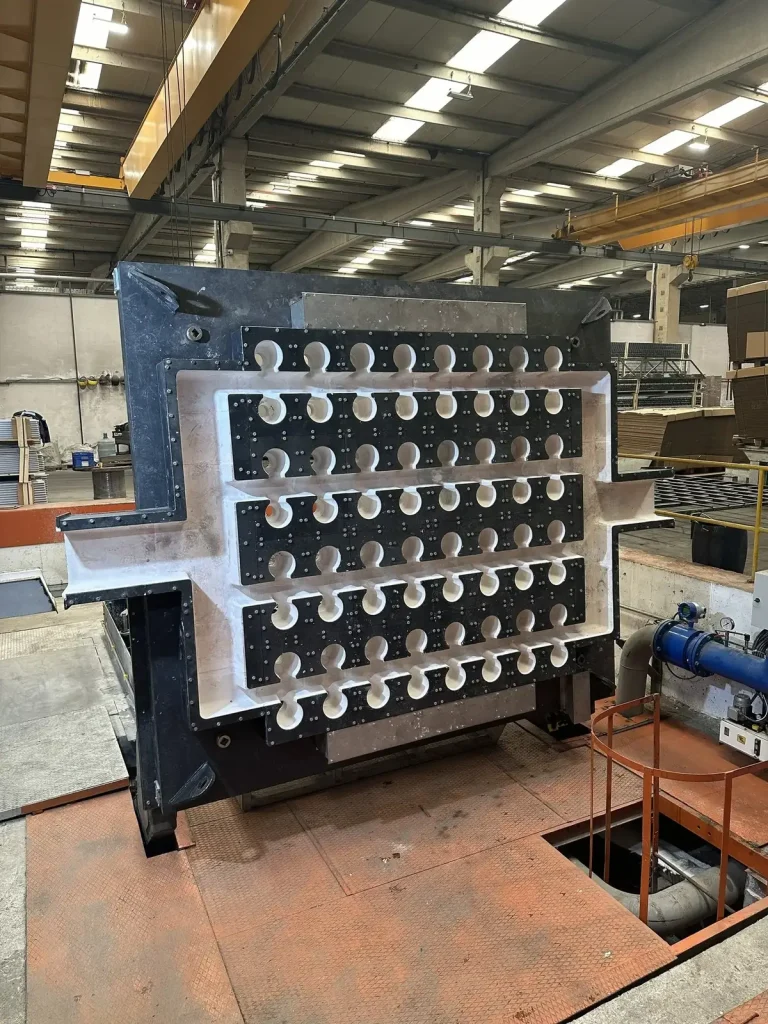
From molten metal to billet
Melting and molten metal preparation
From the charge entering the furnace until the metal is ready for casting. Furnace size and combustion system are calculated together with your charging regime: how many times per shift the furnace is charged and how long it stays closed are inputs to the design.
- Melting furnace
- Holding furnace
- Degassing unit
- Metal quality and refining
- Charging and cleaning systems
Casting and post-casting
The steps in which the metal becomes billet and its thermal history is written. The homogenising furnace is engineered together with the casting line; when the two are considered separately, either the billet waits for the furnace or the furnace stands empty.
- Billet casting systems
- Homogenising furnace
- Ultrasonic testing (UT) systems
- Automatic billet cutting
- Automatic loading & unloading
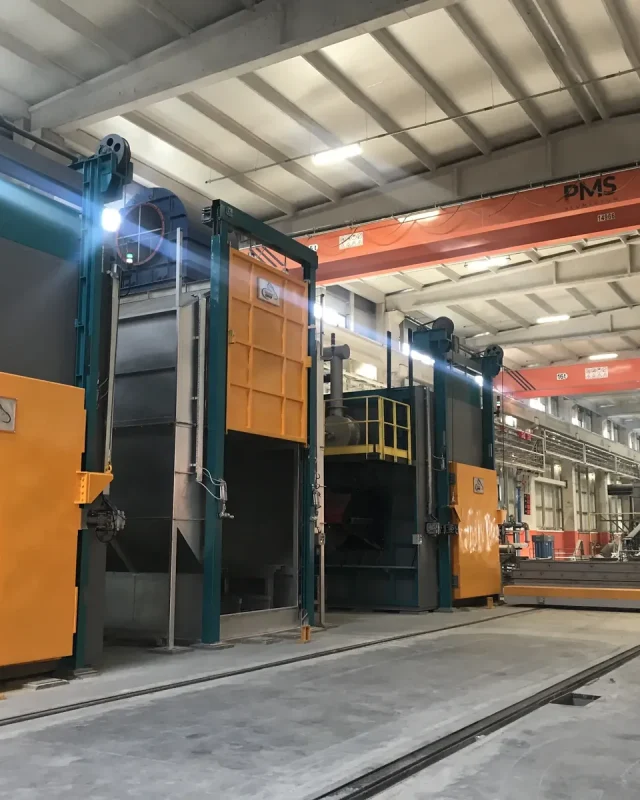
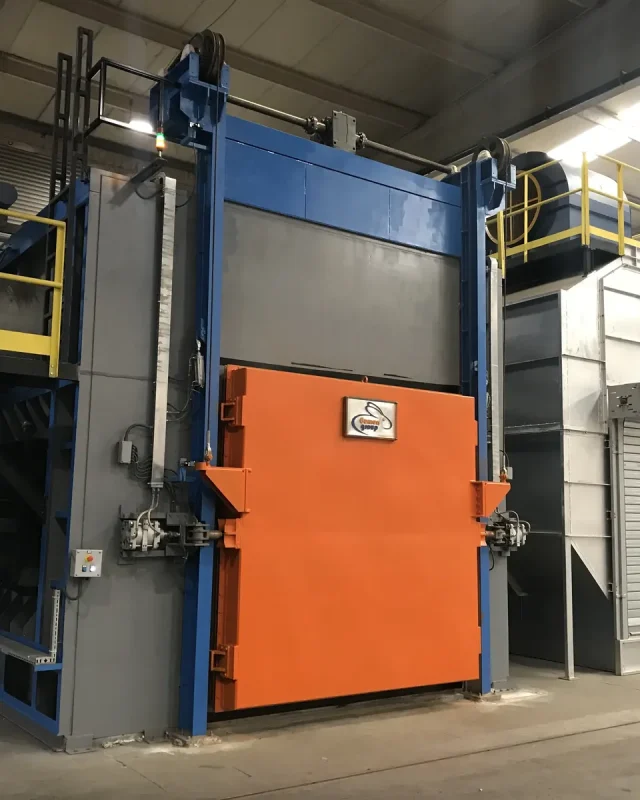
Work we have completed on casting lines
We answer frequently asked questions
about casting and billet production
Melting and holding furnaces, degassing and filtration, the vertical direct chill (VDC) casting machine, homogenisation, billet cutting and ultrasonic testing, and loading and unloading automation — the whole line from furnace to stack, or the steps you choose, under single-source responsibility.
In order: the melting regime and the stability of the holding temperature, removal of hydrogen by degassing and of inclusions by filtration, mould technology (Air-Casting improves surface quality) and the homogenisation cycle. A defect most often originates one step before the one where it becomes visible.
Yes. Single stations such as a degassing unit, a cutting machine or a cooling unit are integrated into the existing line; the deciding factors are the site dimensions and the control interface. After a site survey we provide the scope in writing.
For structures such as the casting pit, we provide the reinforced concrete design and the layout plan; the plant carries out the construction with its own contractor. Mechanical installation and commissioning are ours.
Let’s plan your casting line together, from furnace to stack
Share your daily tonnage, your alloy list and your site dimensions, and we will work out together which steps of the line you need.
Request a Quote