






We equip flat-rolled production both before and after the rolling mill
We build the homogenising furnaces that prepare the slab for hot rolling and the annealing furnaces that bring the coil to its final temper. Both directly determine the mechanical properties and surface quality of the product; atmosphere control and ramp accuracy are at the heart of the design.
The inside and the outside of the coil must see the same temperature
In coil annealing the difficulty is not reaching temperature but holding every layer of the winding at the same temperature. If the outer wraps heat up while the inside lags behind, the properties of the material that comes out vary along the coil. That is why the furnace’s air circulation, load arrangement and cycle time are calculated for the product thickness and coil size — in foil annealing, removal of the oil is also part of the same cycle.
The other end is the melting and casting side at the head of the line. At the Panda Aluminium plant in Ankara, on the melting and holding furnaces of the sheet casting line, we carried out a combustion system refurbishment and automation work; the furnaces were not replaced, the combustion side and the control system were overhauled, and the existing equipment was kept in working order. New investment is not always the only solution.
Explore the Panda Aluminium project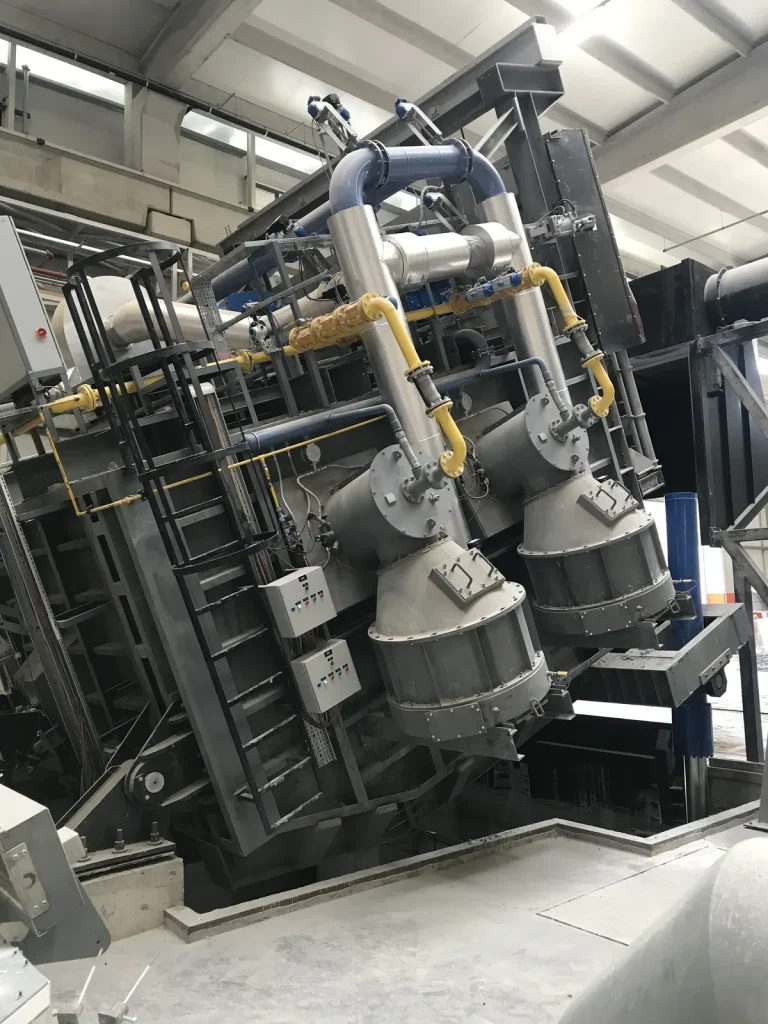
From slab casting to coil annealing
Melting and slab casting
The head of the line. In most plants, renewing the combustion and control side of the existing furnaces gives faster results than a new furnace; we do both.
- Melting and holding furnaces
- Combustion system refurbishment
- Degassing unit
- Casting systems
- PLC & SCADA line control
Heat treatment and annealing
The furnaces on both sides of the rolling mill. Load arrangement and air circulation are calculated for the product thickness; coil handling and charging automation are designed together with the furnace.
- Homogenising furnace
- Sheet annealing furnace
- Foil annealing furnace
- Coil handling and charging systems
- Refurbishment, modernisation and capacity increase
Work we have completed in sheet production
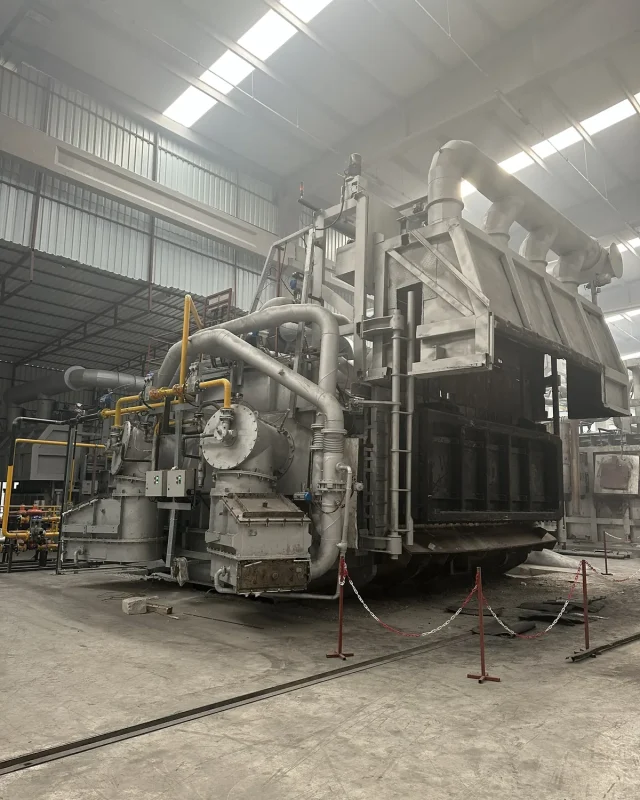
Panda Aluminium
AnkaraCombustion system refurbishment and automation were carried out on the melting and holding furnaces of the aluminium sheet casting line.
DISCOVERWe answer frequently asked questions
about sheet and foil production
Homogenising furnaces that prepare the slab for hot rolling, and annealing furnaces that bring the coil to the target temper after rolling: bell-type for coils, batch-type for sheet packs, continuous for in-line annealing.
Through atmosphere control. Annealing runs very close to the limit for surface quality: a coil annealed in the wrong atmosphere comes out dull and stained even if it is mechanically correct. Dew point monitoring, sealing and oil removal are part of the design.
Annual tonnage and product mix decide. At high and steady tonnage a continuous line takes the lead; where the product mix is wide and the batches are small, bell-type gives flexibility. We make the decision with you, based on your coil dimensions and tonnage.
Yes, if the body and the sealing are suitable. Usually the atmosphere line, the analysis equipment and the control side are renewed, and the furnace body stays. After a site survey we provide the scope in writing.
Let’s define your annealing and homogenisation needs together
Share your coil dimensions, alloys and annual tonnage, and we will choose between a bell-type, batch-type or continuous furnace according to your product mix.
Request a Quote