






We build the furnace side of the extrusion line
We deliver, from a single source, the heating furnace that brings the billet to the right temperature in front of the press, the heat treatment furnace that ages the profile behind it, and the handling automation in between. The furnaces at the two ends directly determine how many metres of profile the press produces per hour.
The billet temperature sets the speed of the press
It is not enough for the billet to leave the furnace merely hot. How the temperature is distributed along its length determines how well the alloy extrudes and the quality of the profile surface; if the furnace cannot hold this, the operator tries to compensate by slowing the press, and the loss comes straight out of tonnage. That is why, when we design the furnace, we look not at nominal capacity but at the real cycle achieved with your alloy and your billet length.
The back of the press is the continuation of the same story. If profiles are carried by hand from the line to the ageing furnace, the line clogs up there. At the AL Metal plant in Konya we connected the end of the line with robotic systems; from exit to stacking, no human hand touches the profile. At the Çuhadaroğlu Metal plant in Istanbul we did not build a new line; we modernised the working line without stopping production — jobs of this kind proceed piece by piece, following the plant’s own shift plan.
Projects we have completed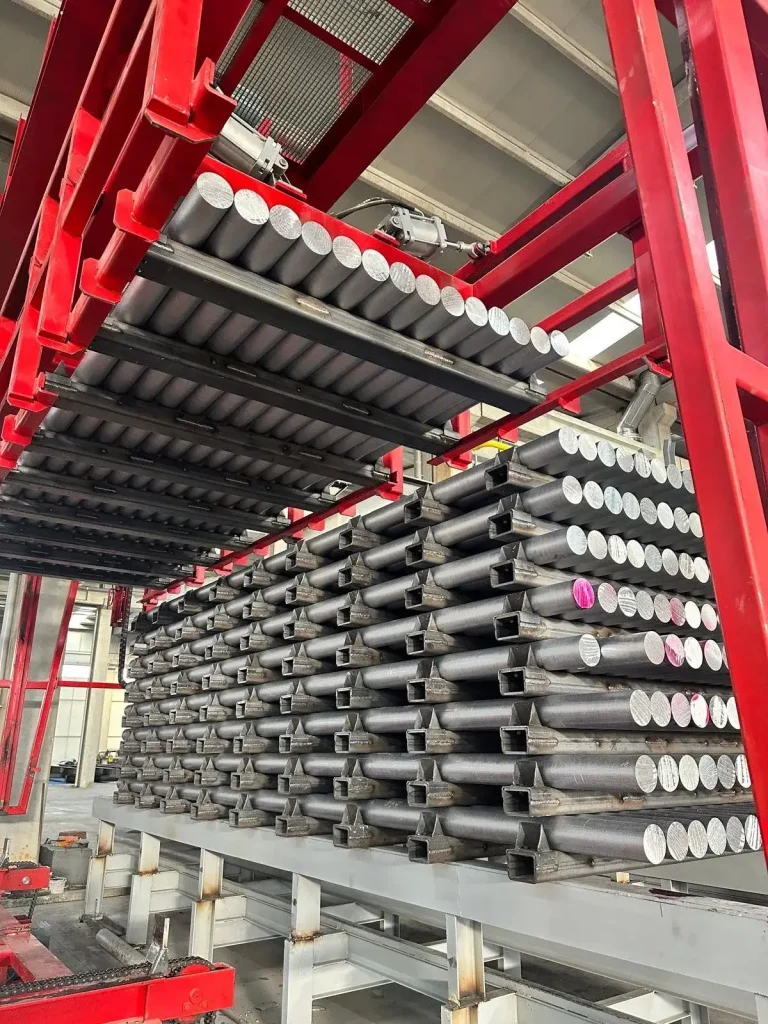
Before and after the press
Before the press
The preparation stations the billet passes through before it enters the press. The furnace, the die side and cutting are engineered as parts of the same flow; equipment selected piece by piece ends up holding each other up on the line.
- Extrusion billet heating furnace
- Die heating furnace
- Automatic billet cutting
- Automatic loading and feeding
- PLC & SCADA line control
After the press
The steps between the profile leaving the press and going on to packaging. In most plants the bottleneck here is not the furnace but the handling; we design the two together.
- Ageing (heat treatment) furnace
- Automatic loading & unloading
- End-of-line stacking and handling
- Drying cabinet and process support systems
- Refurbishment, modernisation and capacity increase
Work we have completed in extrusion plants
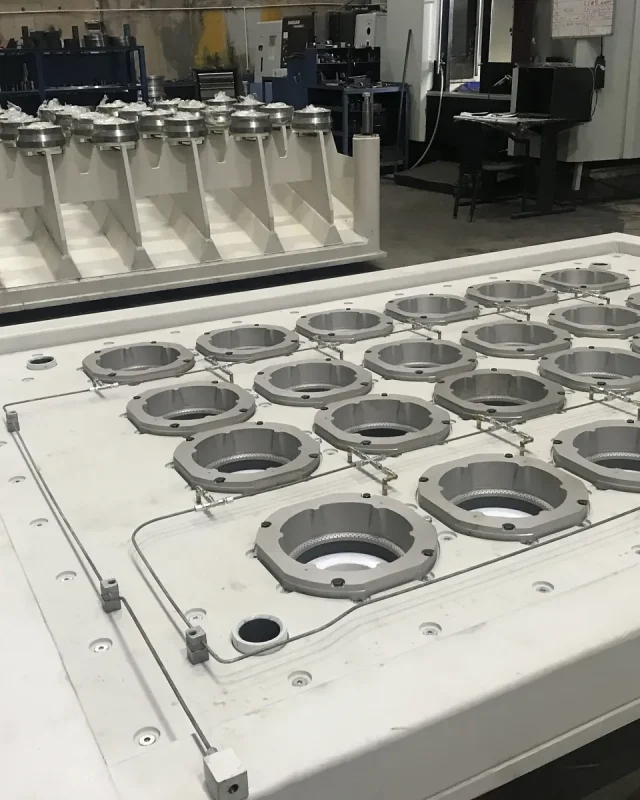
Alfa Metal Aluminium
IstanbulBillet cutting and line integration solutions were provided.
DISCOVER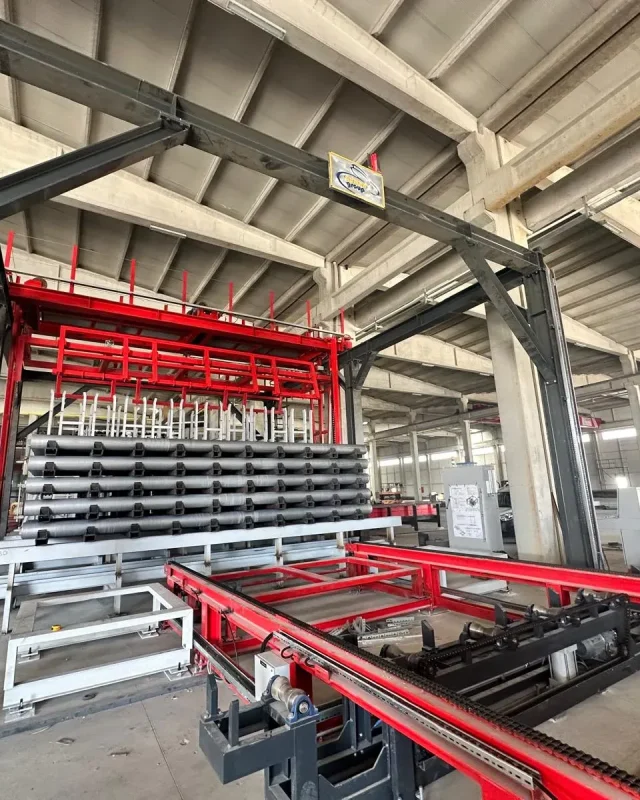
AL Metal Aluminium
KonyaRobotic end-of-line and automation systems supporting the production flow were installed.
DISCOVER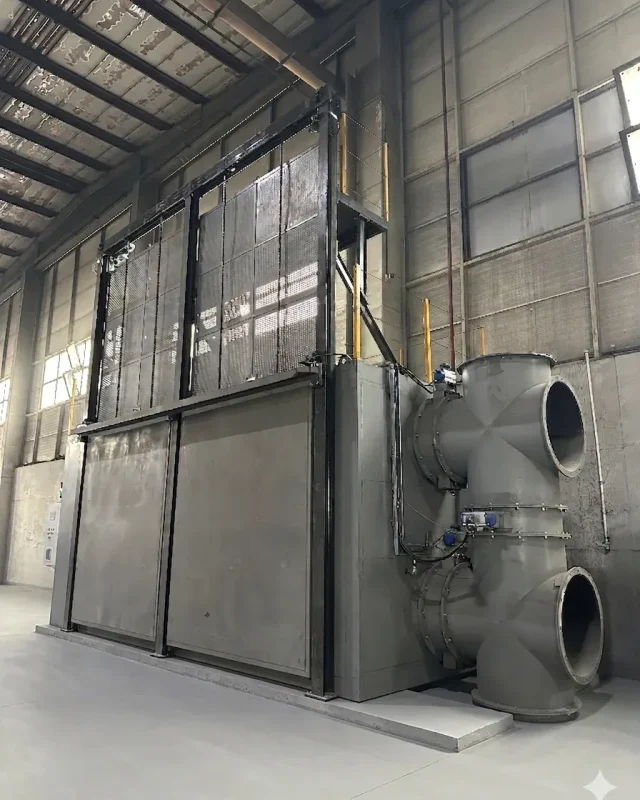
GNS Aluminium
TekirdağA drying cabinet and related process support systems were installed.
DISCOVERWe answer frequently asked questions
about extrusion plants
Billet heating and die heating furnaces in front of the press, an ageing furnace behind it, and billet transfer and end-of-line automation in between. We build the whole heat and handling side of the line, except the press itself.
In continuous, high-tonnage operation a regenerative gas-fired furnace is usually more economical to run; on presses that change products often, induction offers quick start-up and a precise gradient. We make the decision with you, based on your press tonnage and profile mix.
Yes. Most plants that apply T5 start with an ageing furnace. The furnace is sized to the elevation of your press run-out conveyor and to your profile length; the layout is planned as though solution treatment will be added later.
We do. The signal exchange needed to synchronise the furnace and the press is defined together with the press manufacturer at the start of the project; at commissioning the two systems are tested together.
Let’s plan the front and the back of your press together
Share your press tonnage, profile mix and target capacity, and we will quote billet heating, ageing and handling automation accordingly.
Request a Quote