






We deliver the vertical casting machine together with its moulds in a single project
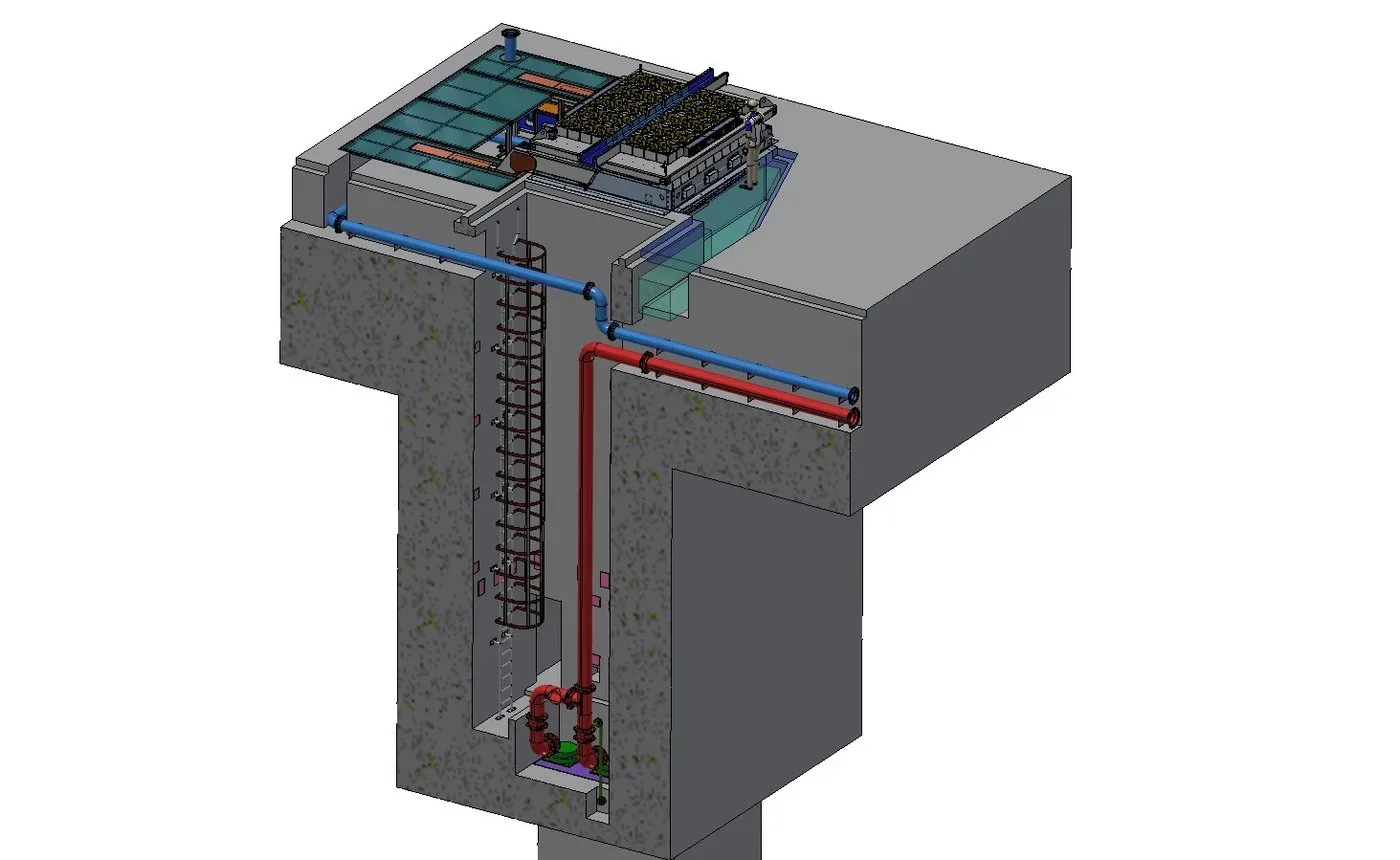
We build the complete VDC line for billet and slab production: the casting table, pit, water distribution system and hydraulic lowering control come out of a single project. We machine the moulds and water distribution heads specific to each billet diameter in our own workshop in Çayırova, and we also supply the reinforced concrete design of the pit.
- Method
- Vertical DC
- Billet diameter
- 75 – 300 mm
- Mould
- Our own manufacture
- Control
- PLC: speed + water
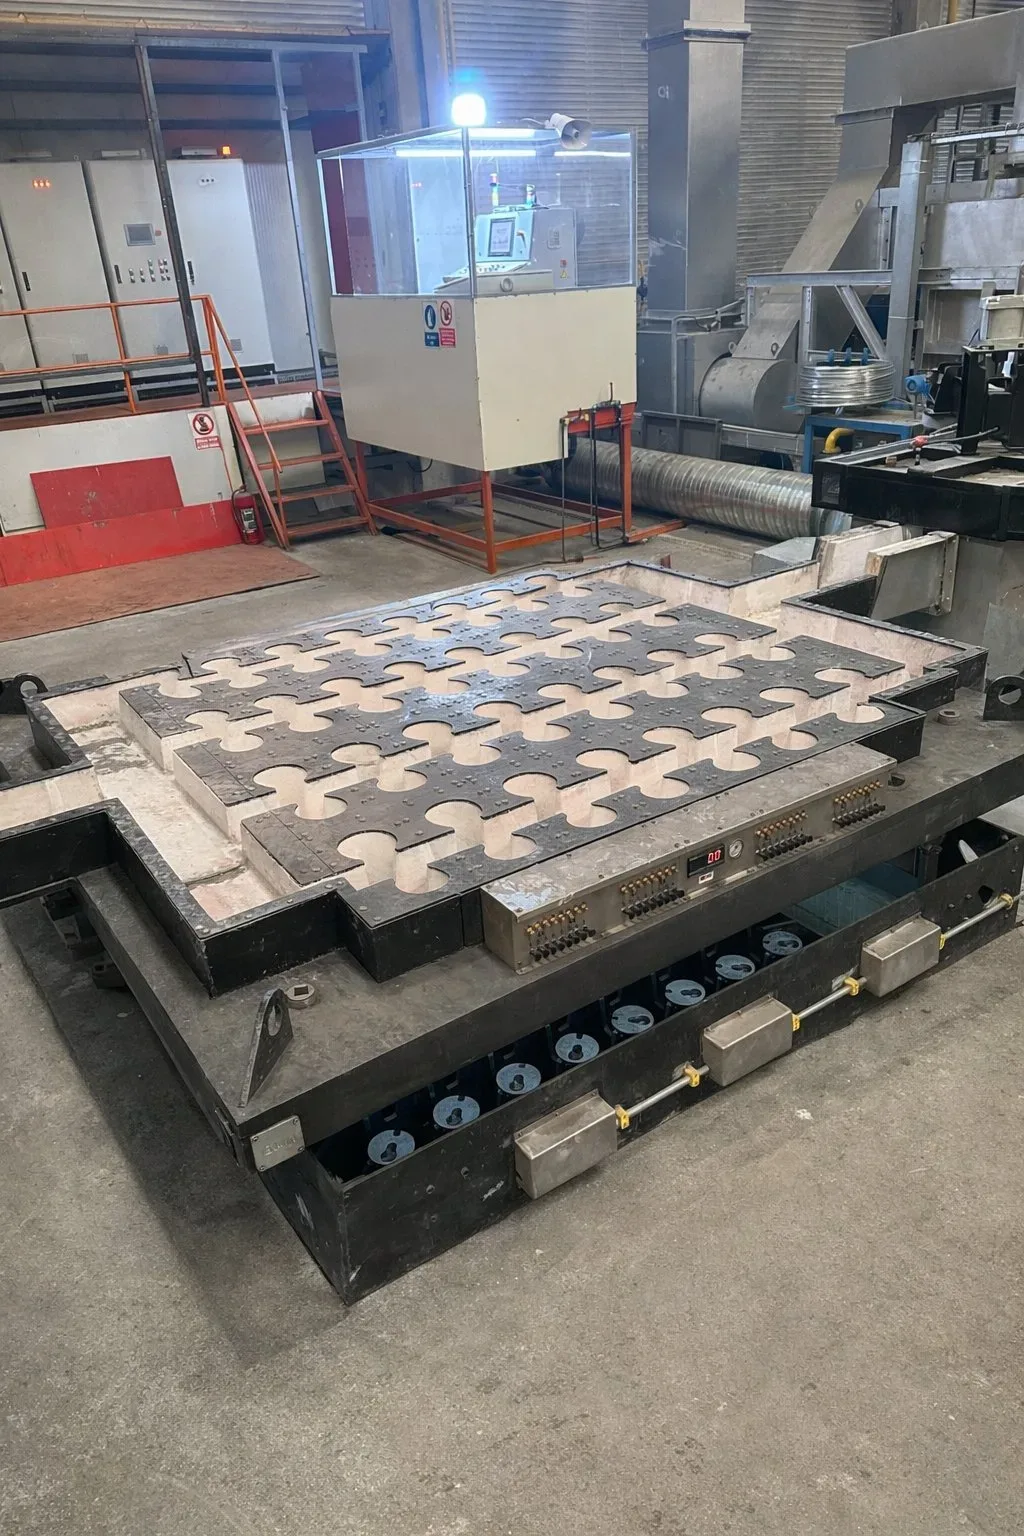
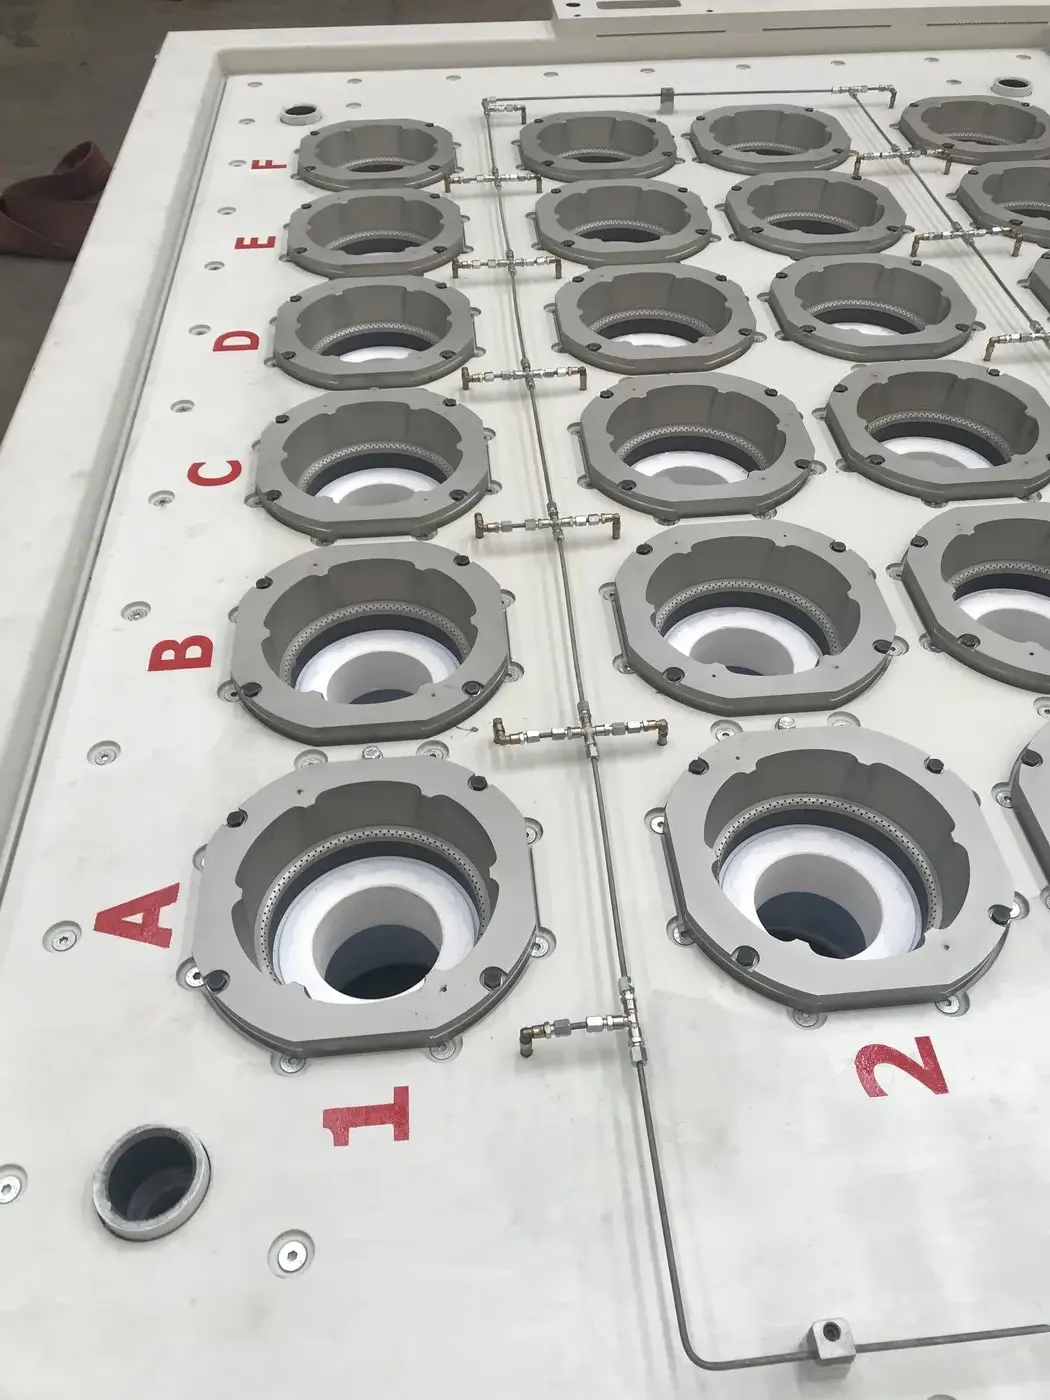
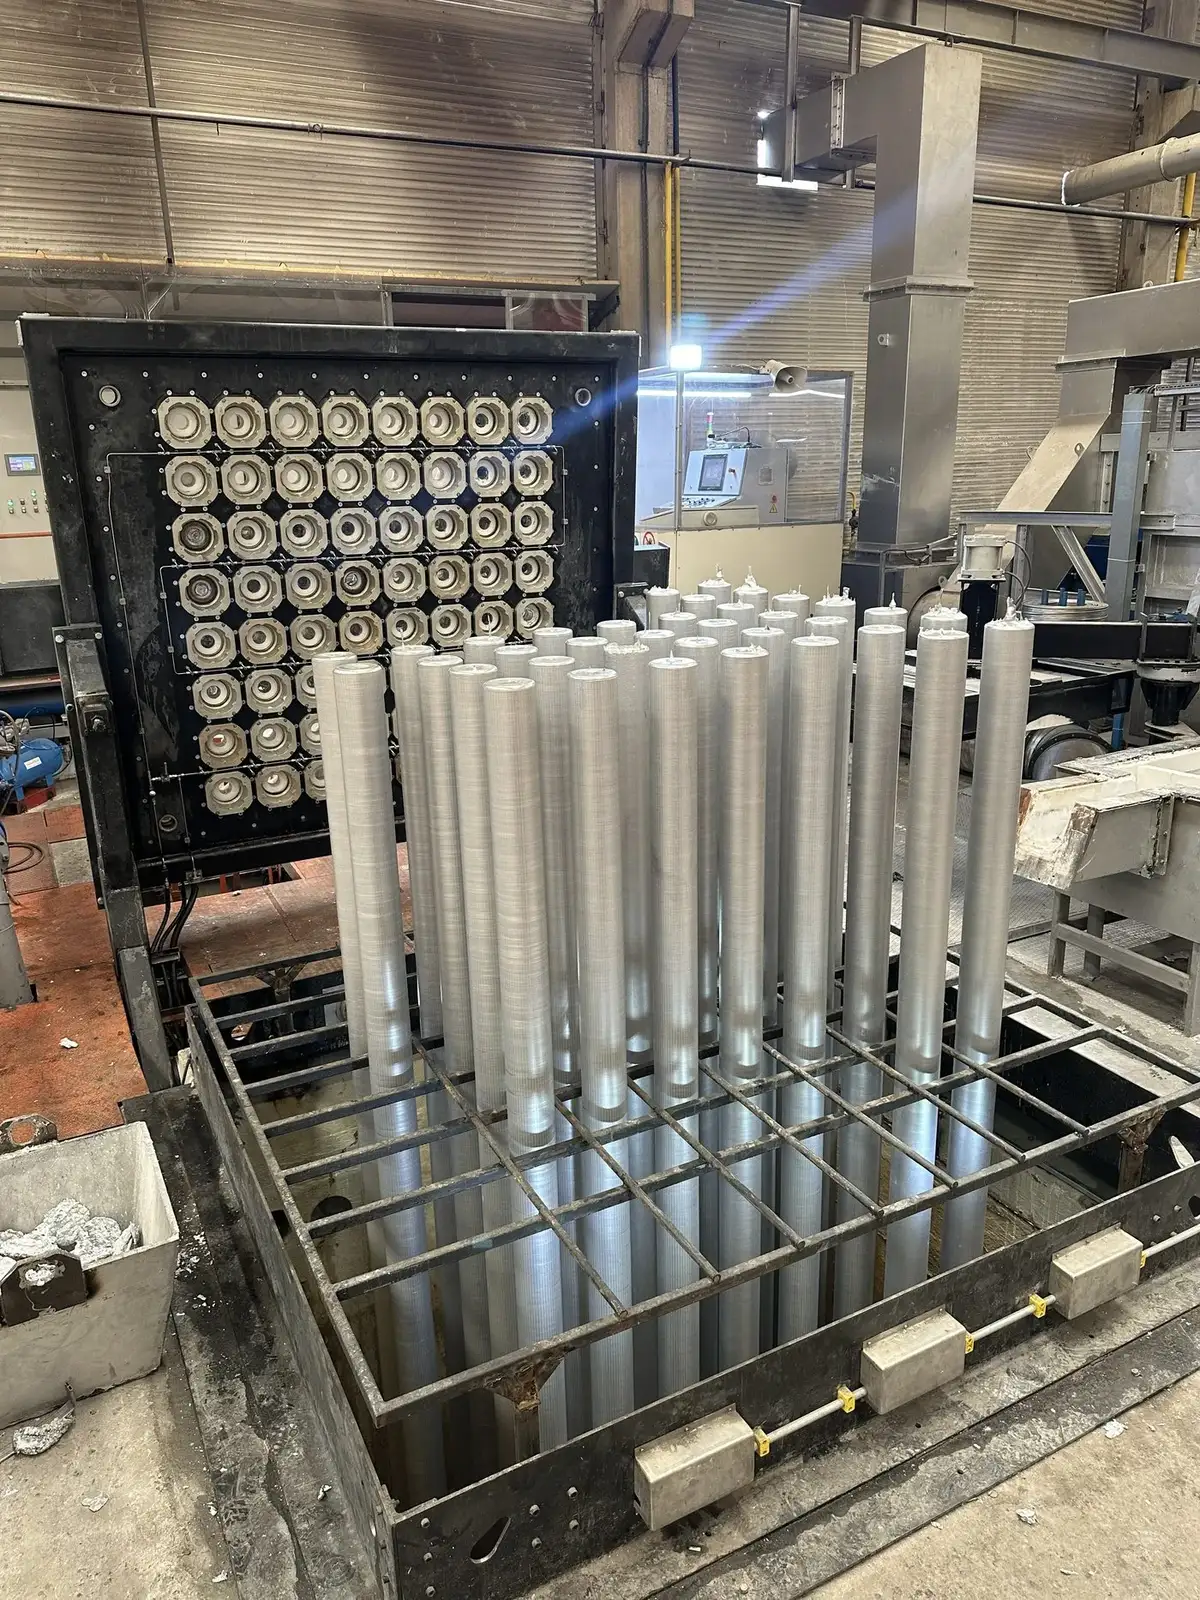
Vertical casting machine (VDC) technical specifications
- Casting method
- Vertical direct chill (VDC) casting
- Billet diameter
- 75 – 300 mm
- Slab cross-section
- Project-specific
- Mould table
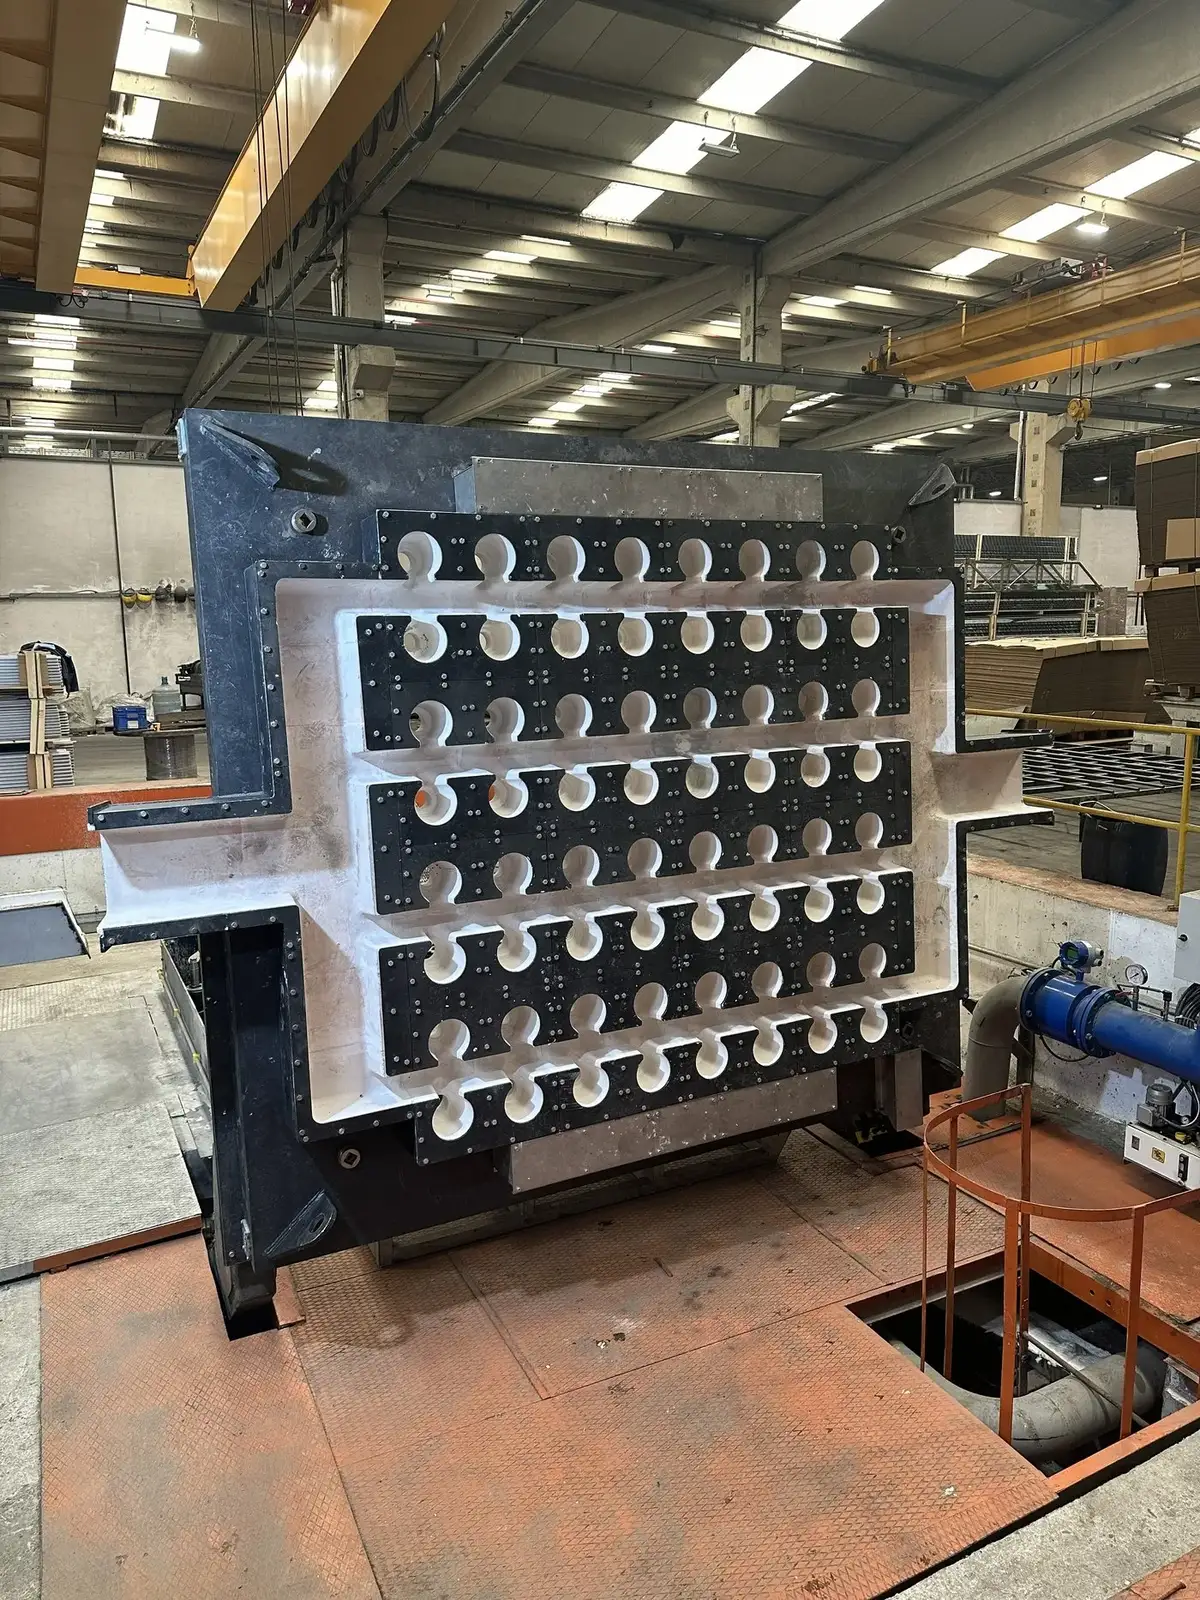
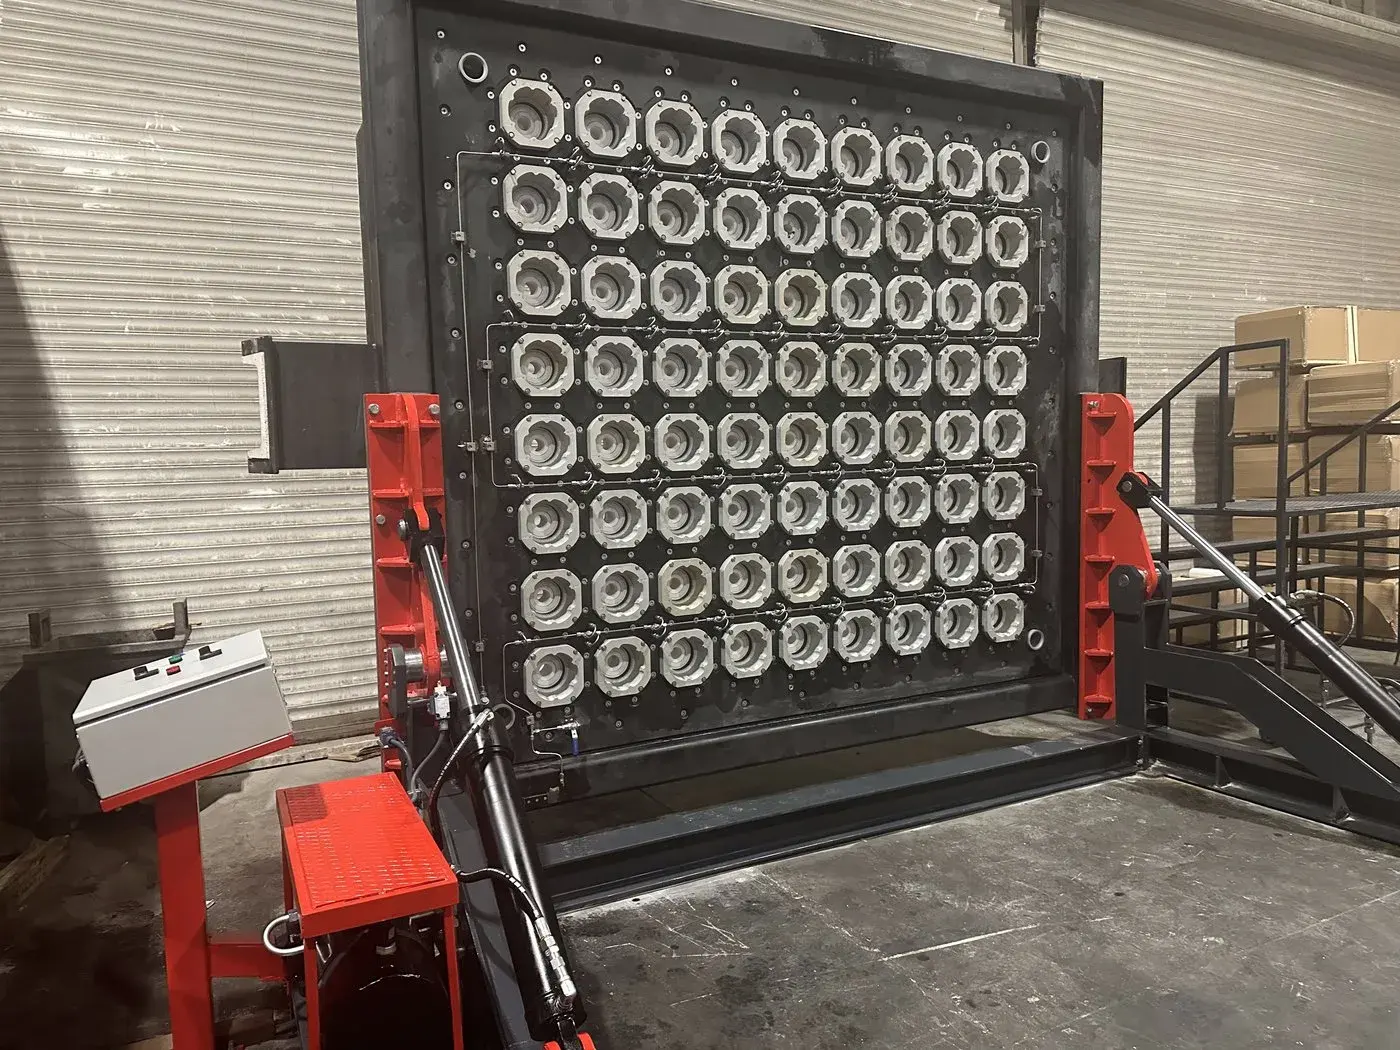
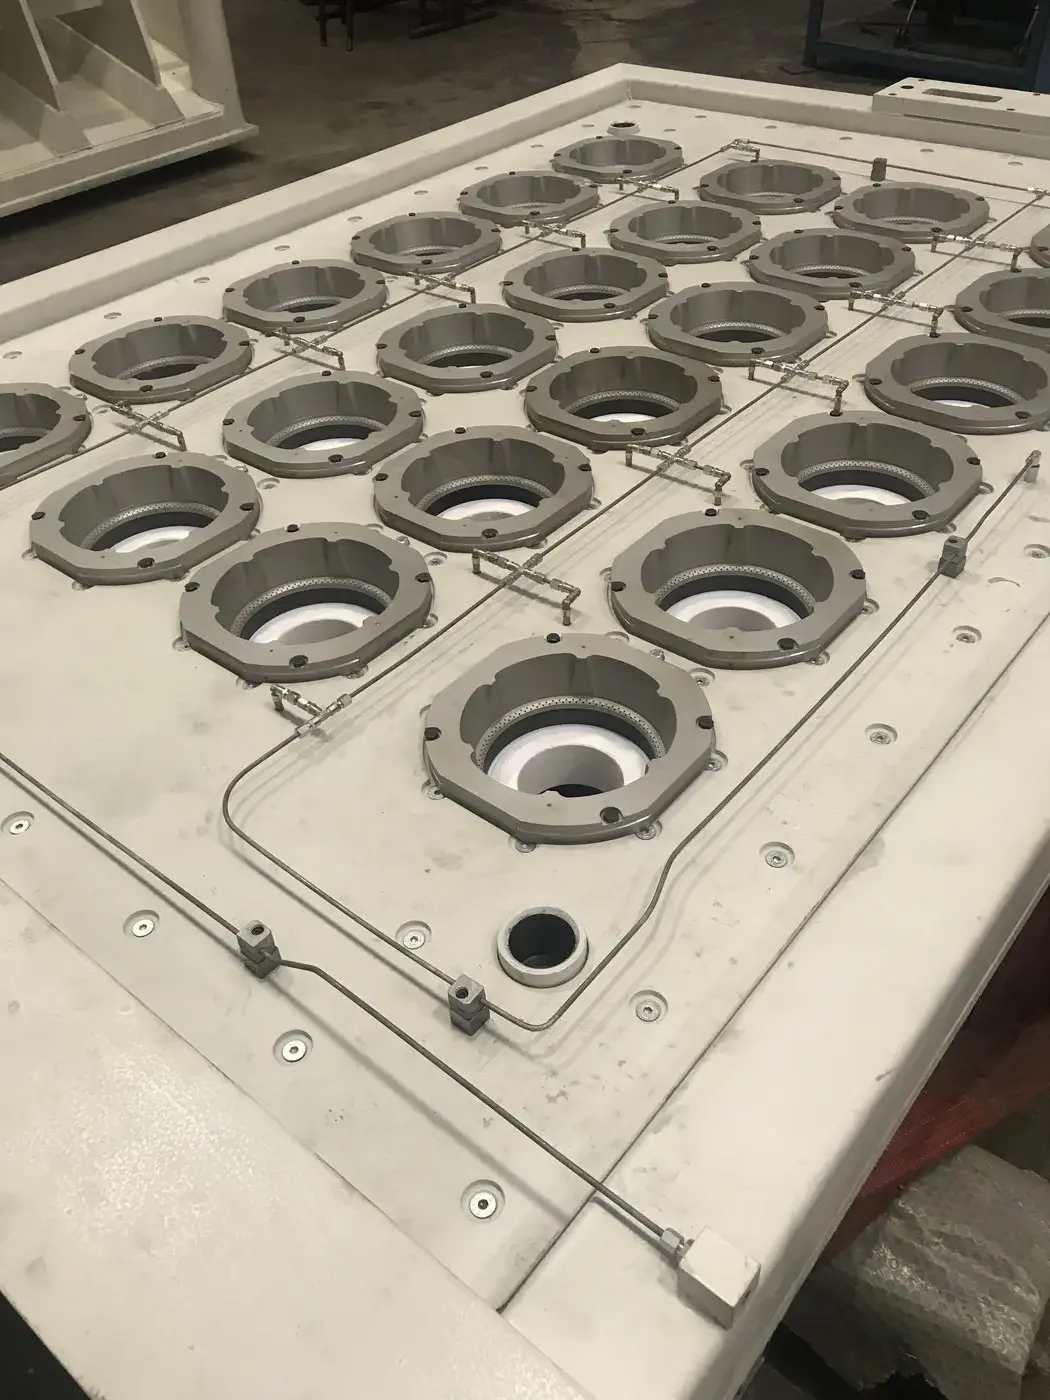
- Multiple mould slots — number of slots depends on diameter and capacity
- Moulds and water heads
- Made by Gumen; specific to billet diameter
- Cooling water
- Closed loop; flow rate PLC-controlled
- Lifting mechanism
- Hydraulic; casting speed is infinitely adjustable
- Control
- PLC: casting speed, water flow rate, level monitoring
- Alloy compatibility
- 1xxx – 7xxx series
- Pit and infrastructure
- Reinforced concrete pit design and layout plan included
- Ultrasonic test
- Optional; integrated into the line
- Reference
- Lines installed in more than 7 countries
What changes when the mould comes from the same place as the machine?
The fit between the mould, the water distribution head and the table directly determines the cast surface. When these three parts come from different suppliers, finding out which one is out of tolerance takes weeks when a problem appears. Because we machine the moulds to billet diameter ourselves, the adjustment time at first commissioning is shorter, and adding a new diameter later is a single item of work.
We build the same machine for billet and for slab
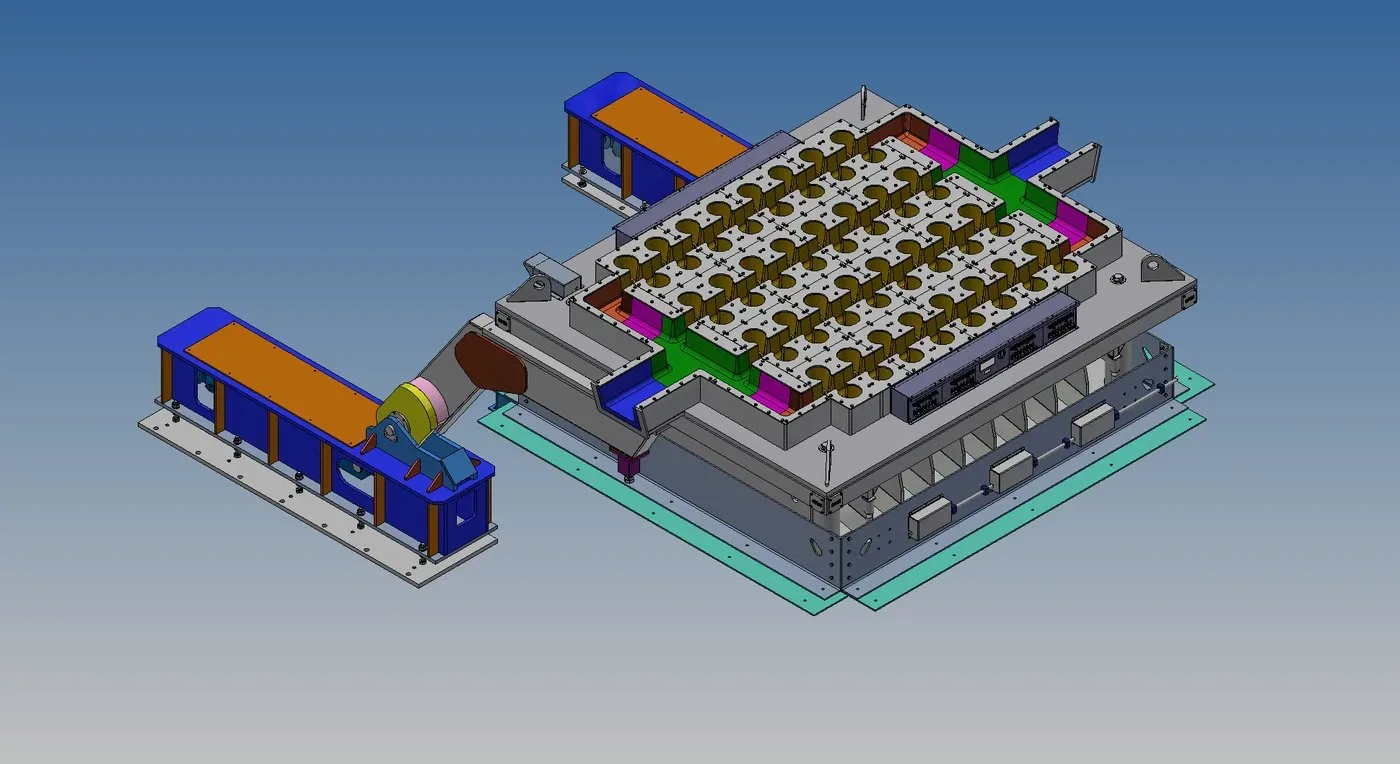
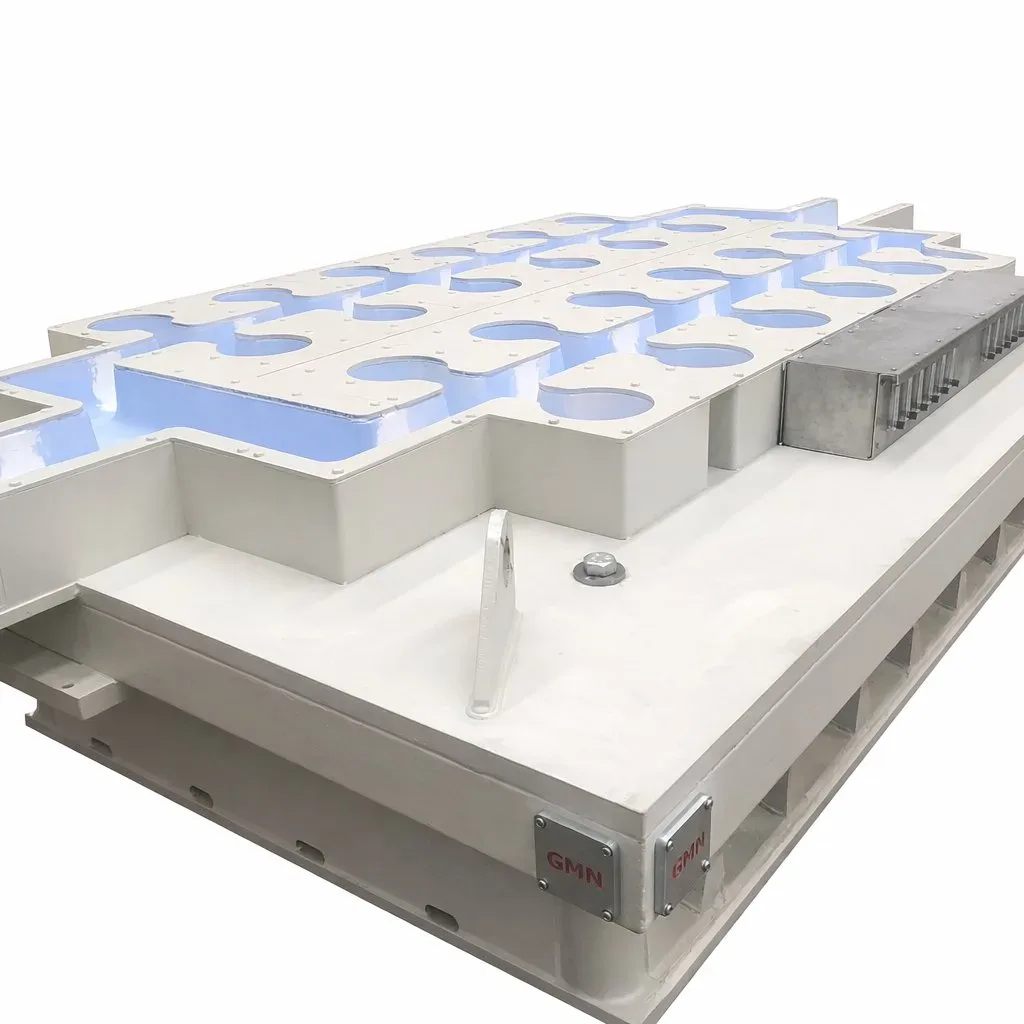
Billet Casting Table
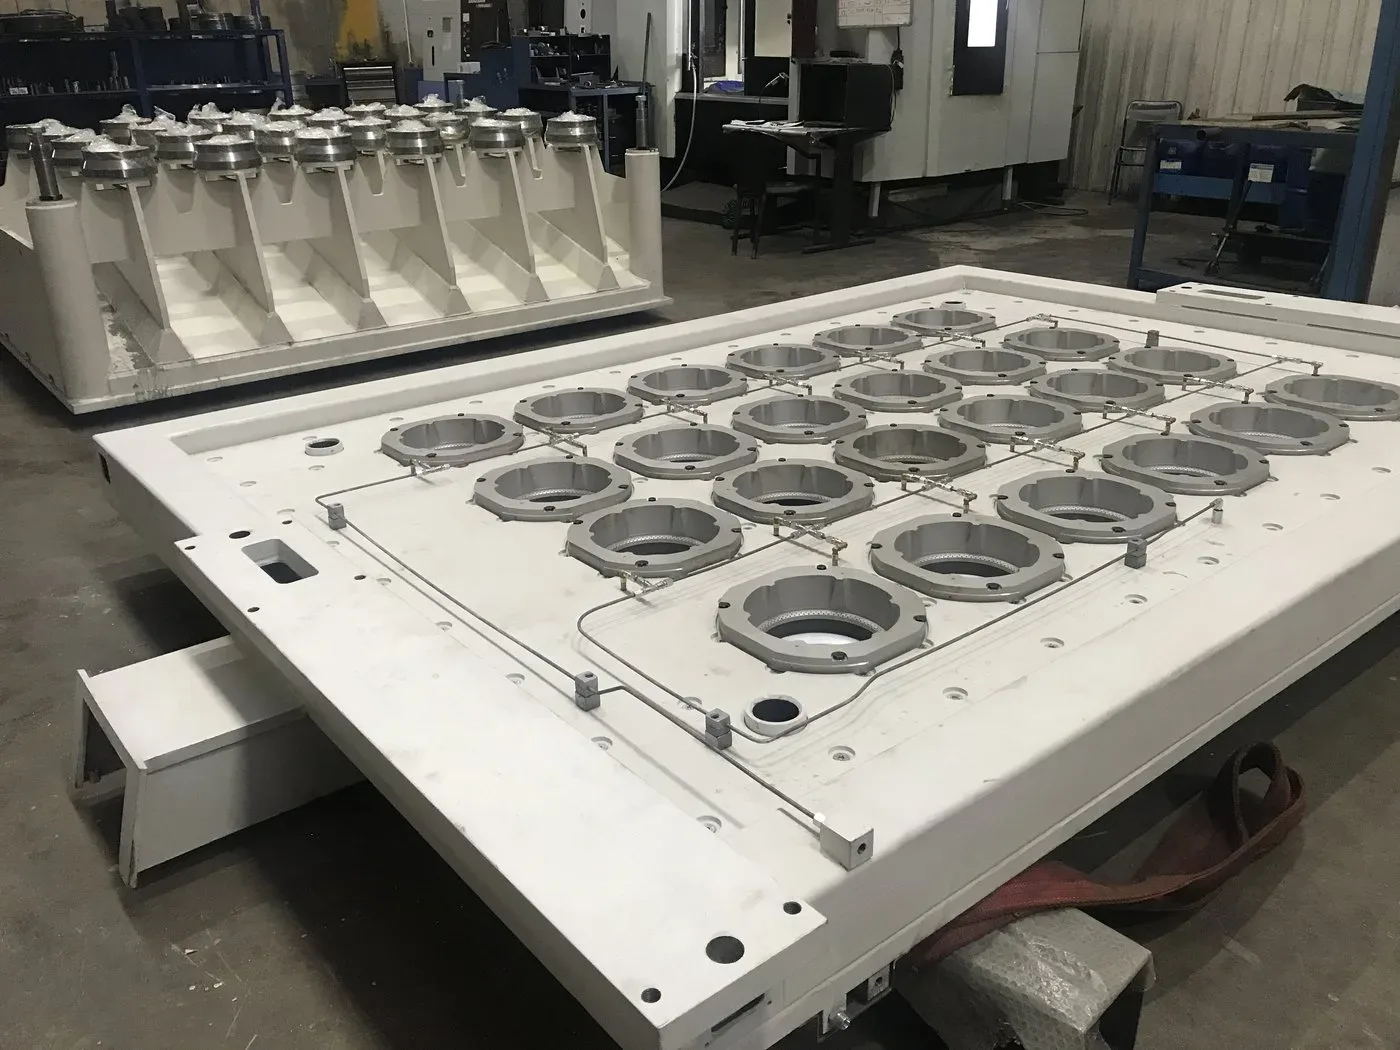
Single-diameter or multi-diameter slots; the number of slots is determined by capacity. The table is sized to the pit opening and the lifting mechanism.
Slab Casting Configuration
The section is project-specific. The mould and water distribution are recalculated for the slab width, and the pit depth is designed accordingly.
In-Line Ultrasonic Testing
Automatic scanning after cutting; details are on the Automatic Saw and UT System page. No separate station is installed; it goes inside the line.
Closed-Loop Water System
The cooling water stays in circulation; losses come only from evaporation and blowdown. Tower capacity is selected according to the casting programme.
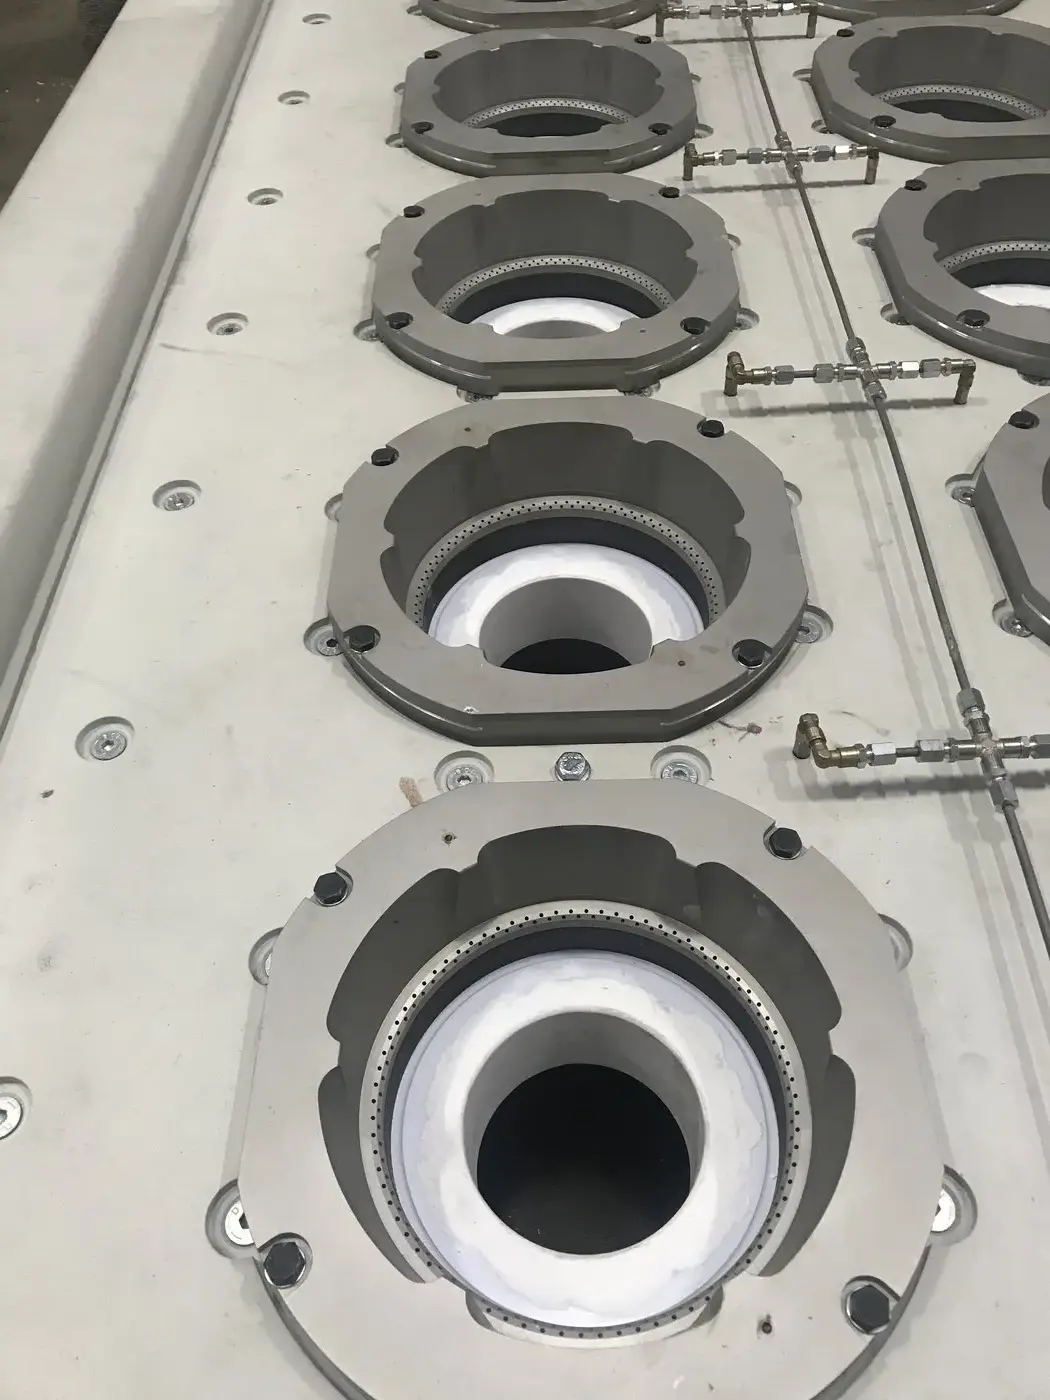
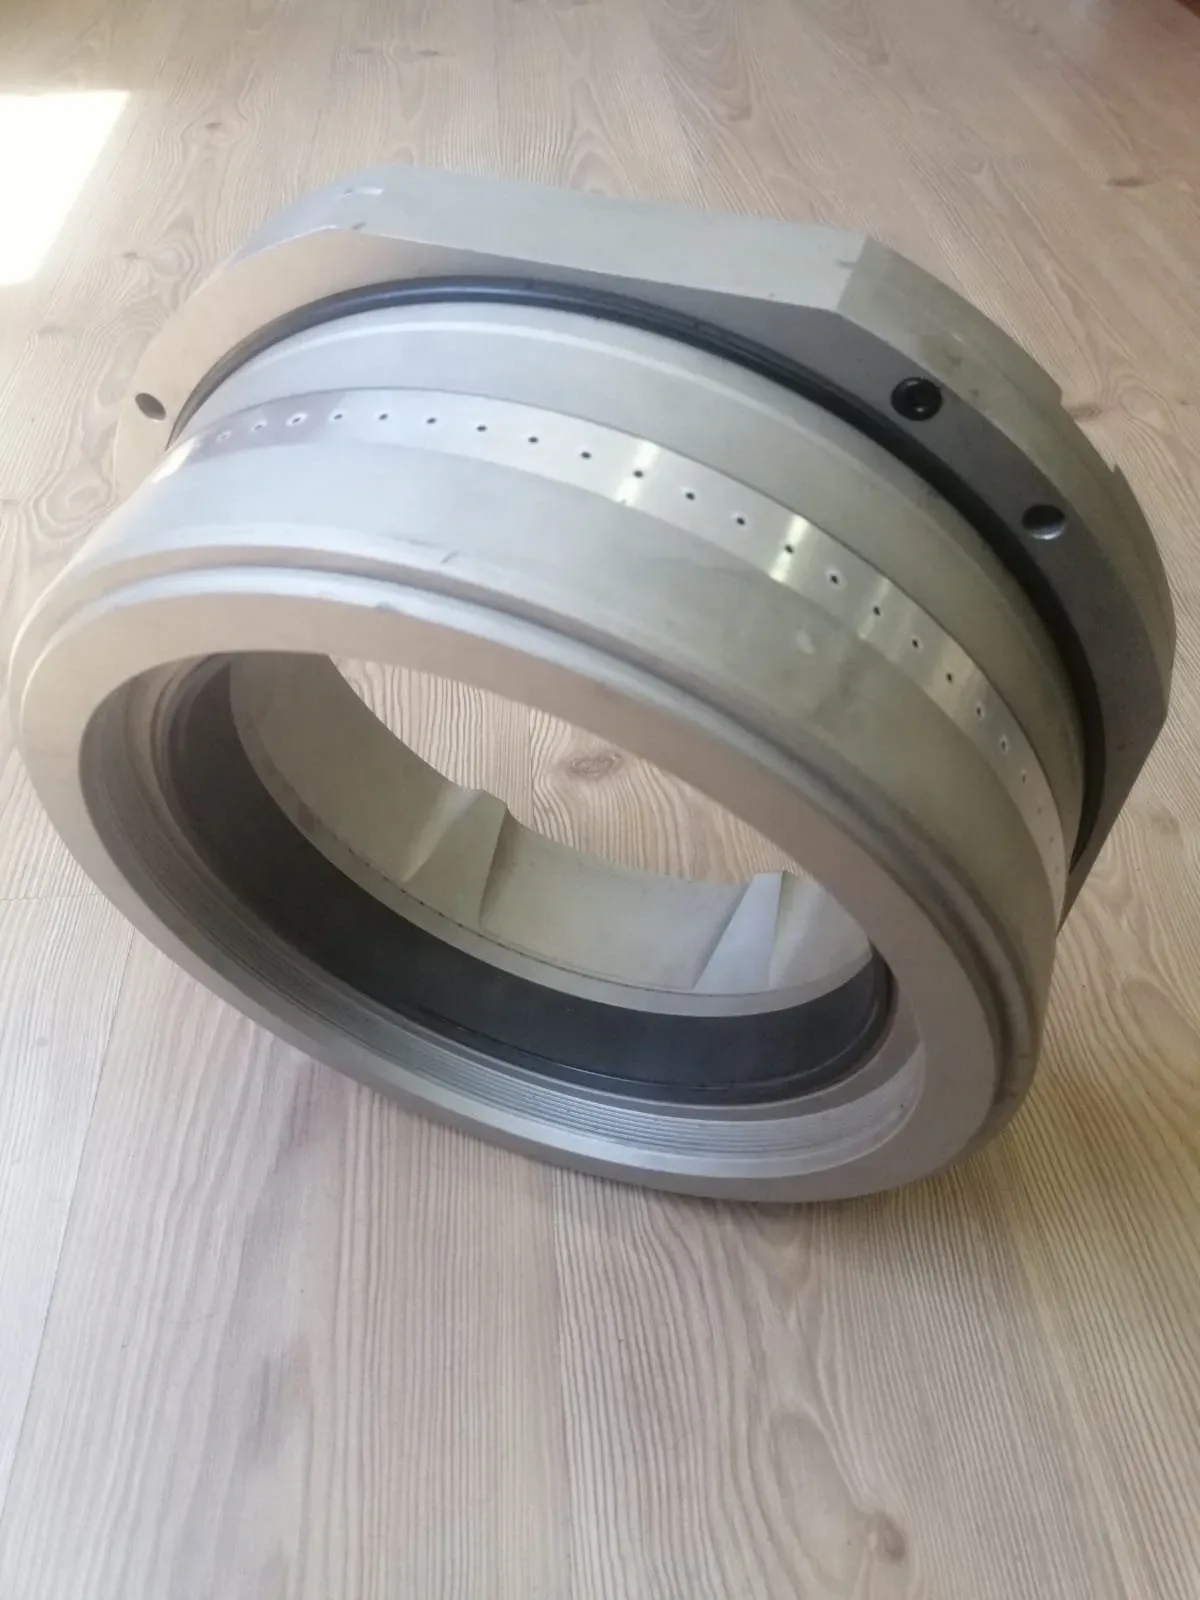
Mould and Water Head Sets
Spare moulds are also manufactured in our own workshop. There is no waiting for import lead times on a critical part.
Four things set this machine apart
A single package, moulds included
Moulds and water distribution heads specific to each billet diameter are machined in our workshop. The casting machine and the mould come from the same place.
We draw up the project starting from the pit
The reinforced concrete pit design, layout plan and mould table installation are part of the same job. No mismatch problems arise on site.
Testing is built into the line
The cut billet is scanned while it is on the line; the result is matched with the casting parameters and archived.
Spare parts sourced domestically
The mould, water head and mechanical assemblies are manufactured in Türkiye. A line that has stopped does not wait for a part at customs.
Explore the technical documents and catalogues

We answer frequently asked questions
about vertical casting
The table can be prepared for more than one diameter by changing the mould slot layout. As the difference between diameters grows, the water distribution has to be rebalanced; we determine at the project stage which diameter groups will work together.
We supply the reinforced concrete design and the layout plan; the plant carries out the construction work with its own contractor. The mould table and mechanical installation are our responsibility.
Yes, if there is enough distance on the transfer line after cutting, and that includes lines made by other manufacturers. After a site survey, we share in writing what will be added.
In a closed-loop system the water stays in circulation; consumption consists only of evaporation and blowdown losses. The net figure is worked out project by project, according to tower capacity and the casting programme.
Which line is this machine part of, and what runs before and after it?
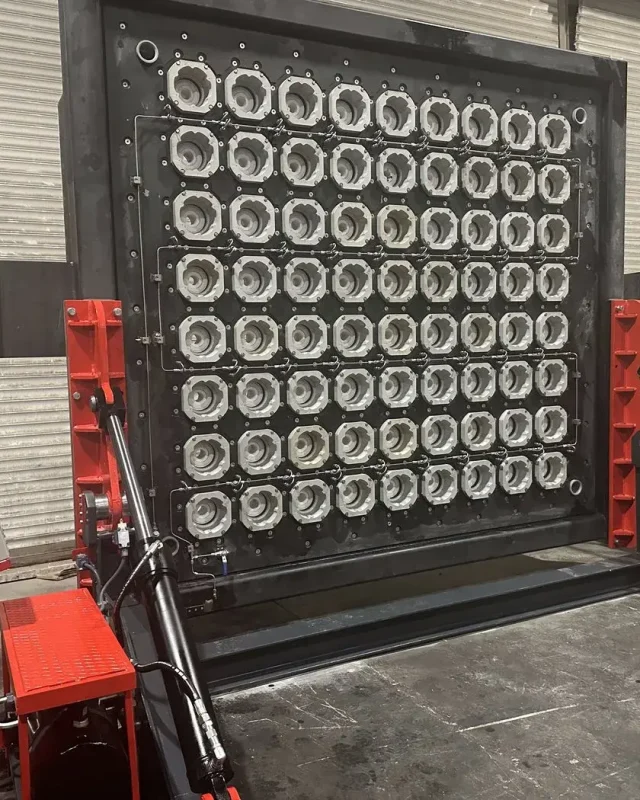
Billet Casting Line
How does the billet surface change when the pit, mould table and water control are built as a single system?
DISCOVER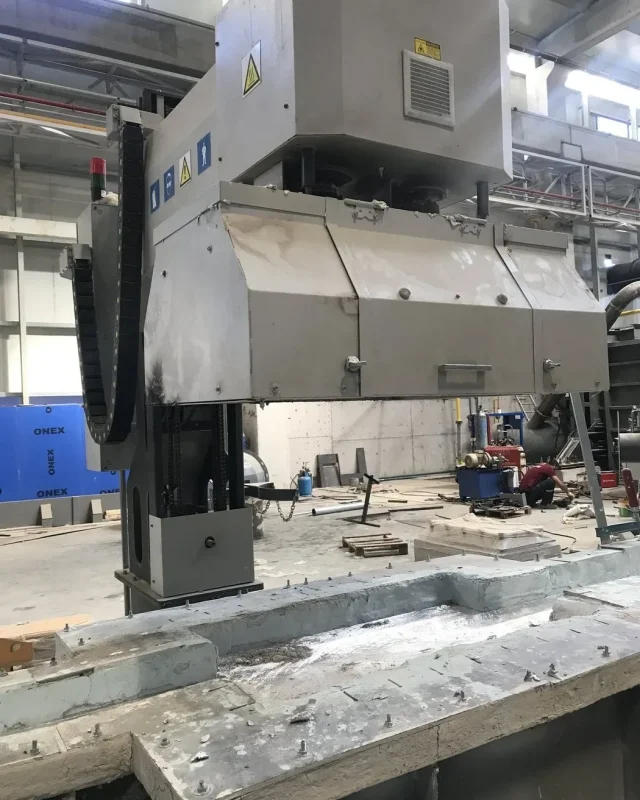
Degassing & Filtration
Hydrogen and oxide residue in the metal entering the mould are removed in the previous unit.
DISCOVER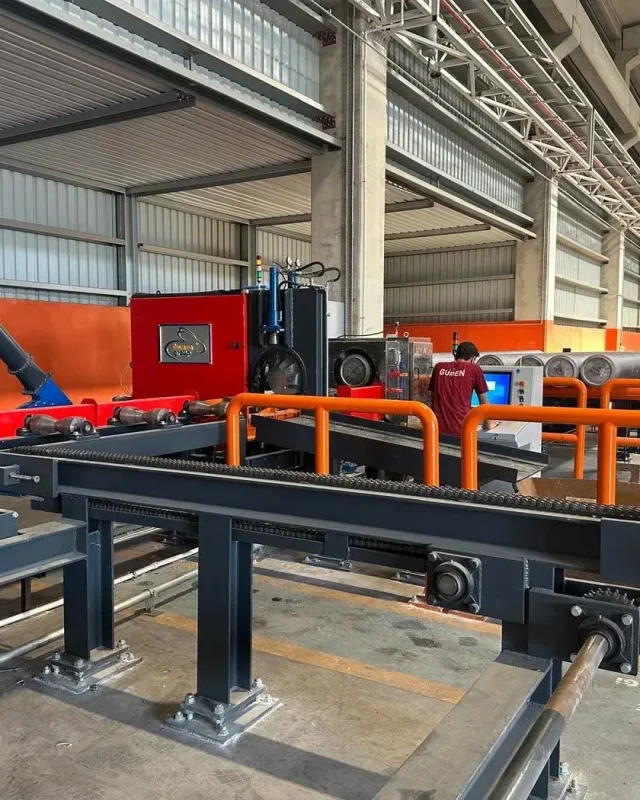
Automatic Saw and UT
The cast billet is cut to length and its interior is scanned, all inside the line itself.
DISCOVER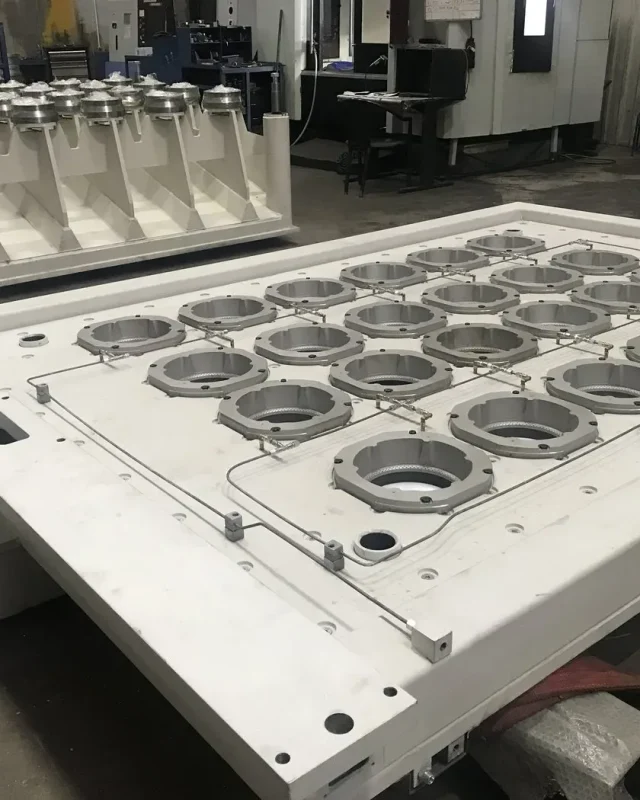
Machine & Parts Manufacturing
The workshop that makes the mould, water head and mechanical assemblies; no waiting for imports of spare parts.
DISCOVERShare your diameter list and we will size the table
Which billet diameters do you cast, what is your daily tonnage, and how much space do you have for the pit? With these three pieces of information, we settle the number of slots, the mould set and the pit design together.
Request a Quote